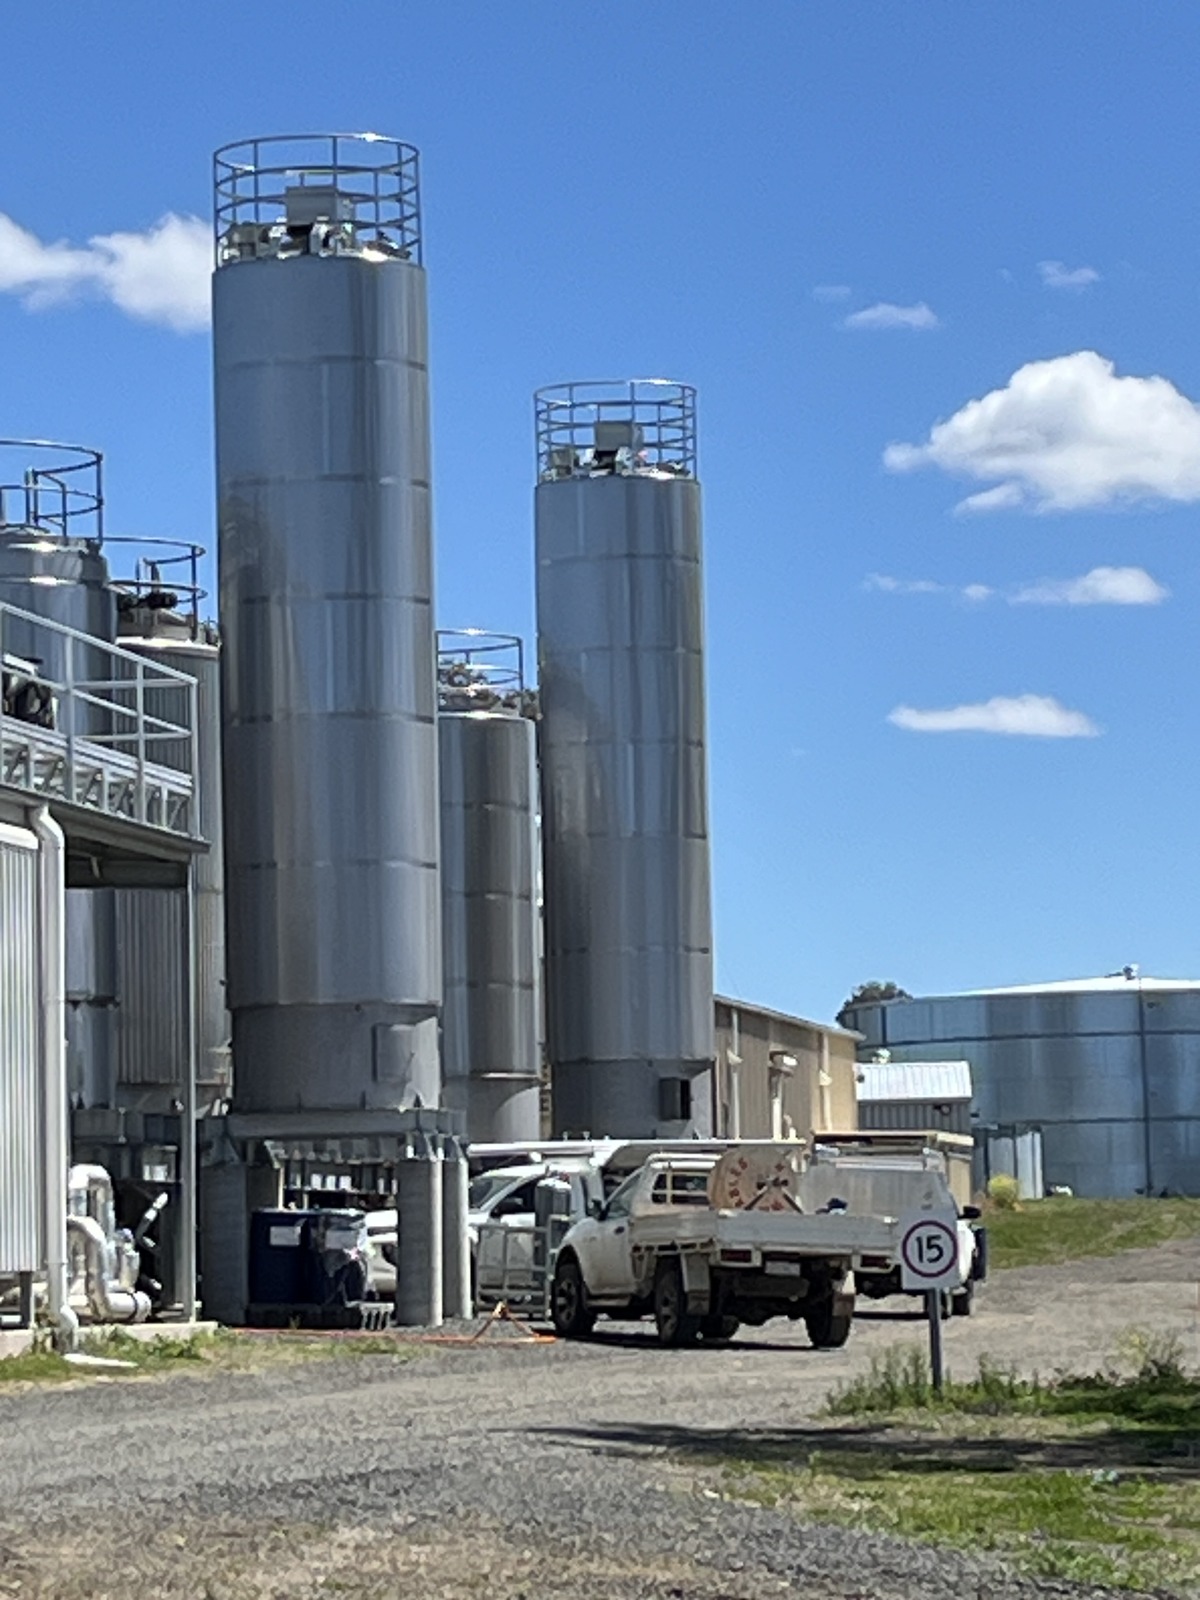
1. The Client Brief & Challenge
An egg processing company in Queensland needed additional storage capacity to support production expansion. Fresh liquid egg required chilled holding, gentle agitation and equipment designed for thorough cleaning.
- Additional capacity: Supply two tanks, each with 20,000 litres of working capacity, to expand egg-holding capacity.
- Temperature and product handling: Provide jacketed storage suitable for glycol cooling, with agitation to help maintain an even temperature and prevent separation.
- Hygienic construction: Use stainless steel construction, carefully finished welds and clean-in-place provision for the egg application.
- Structural design: Engineer the tank supports and vessel construction for the substantial filled load.
2. The Process Plant Network Solution
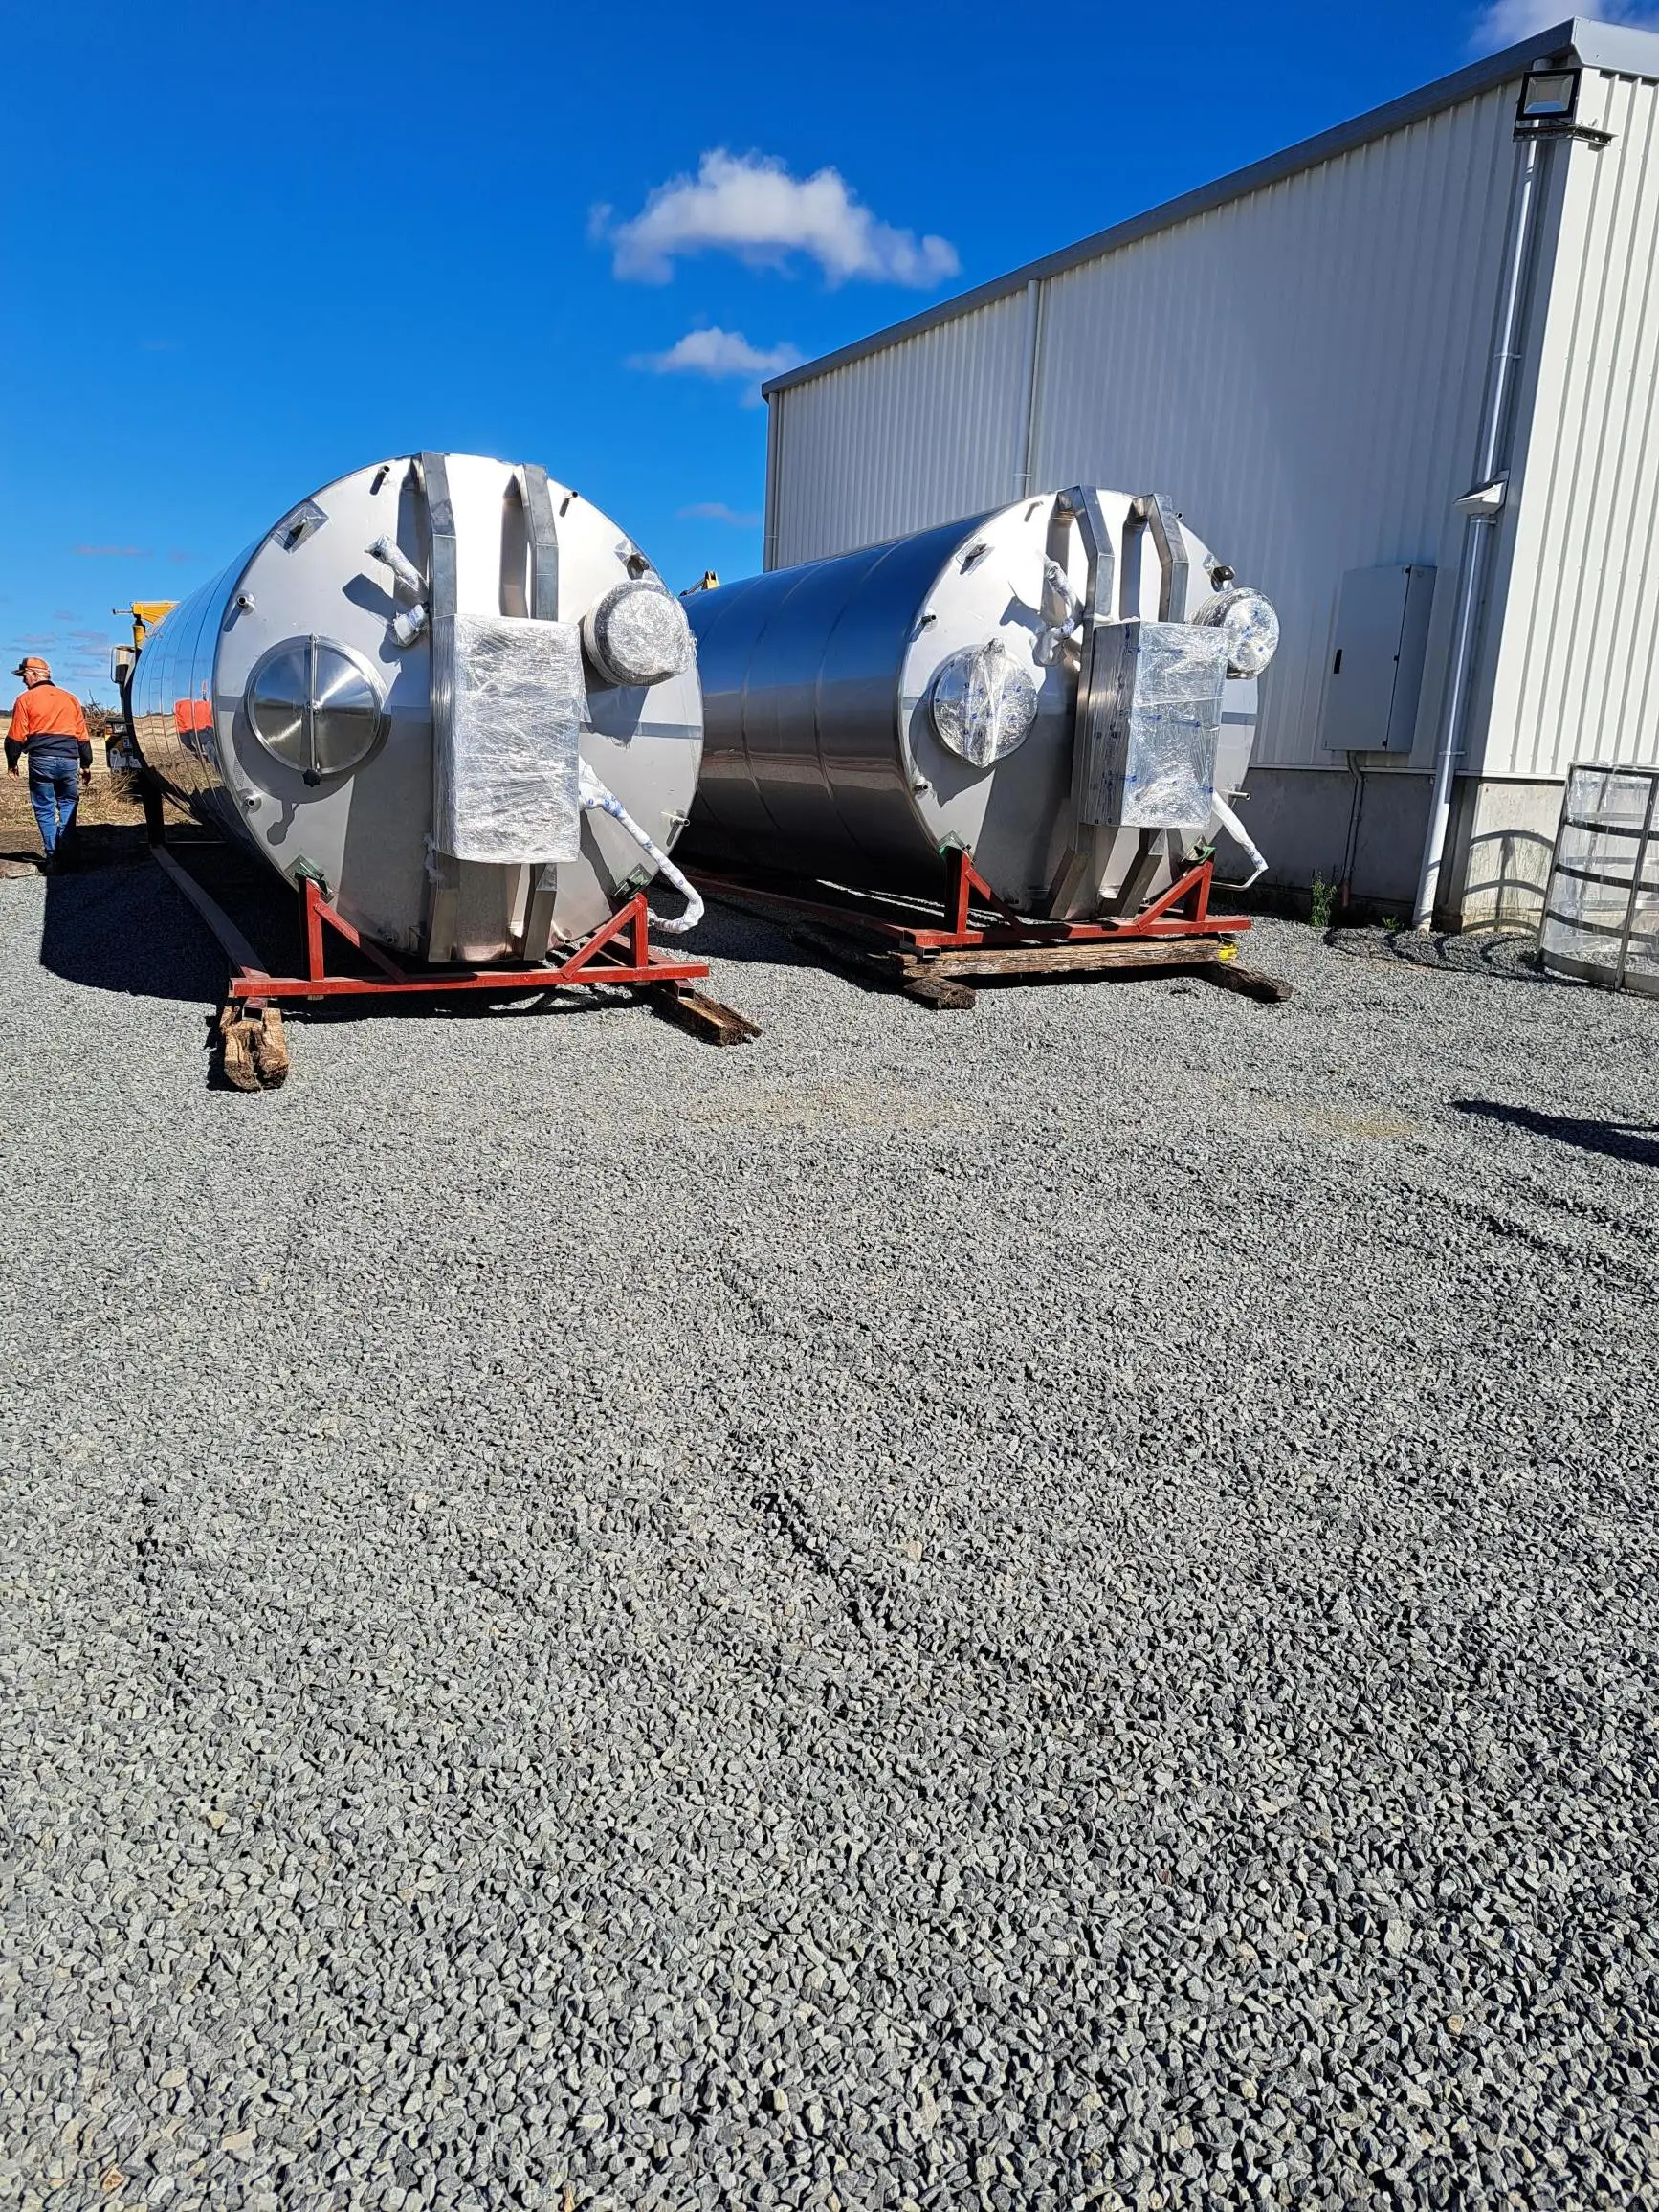
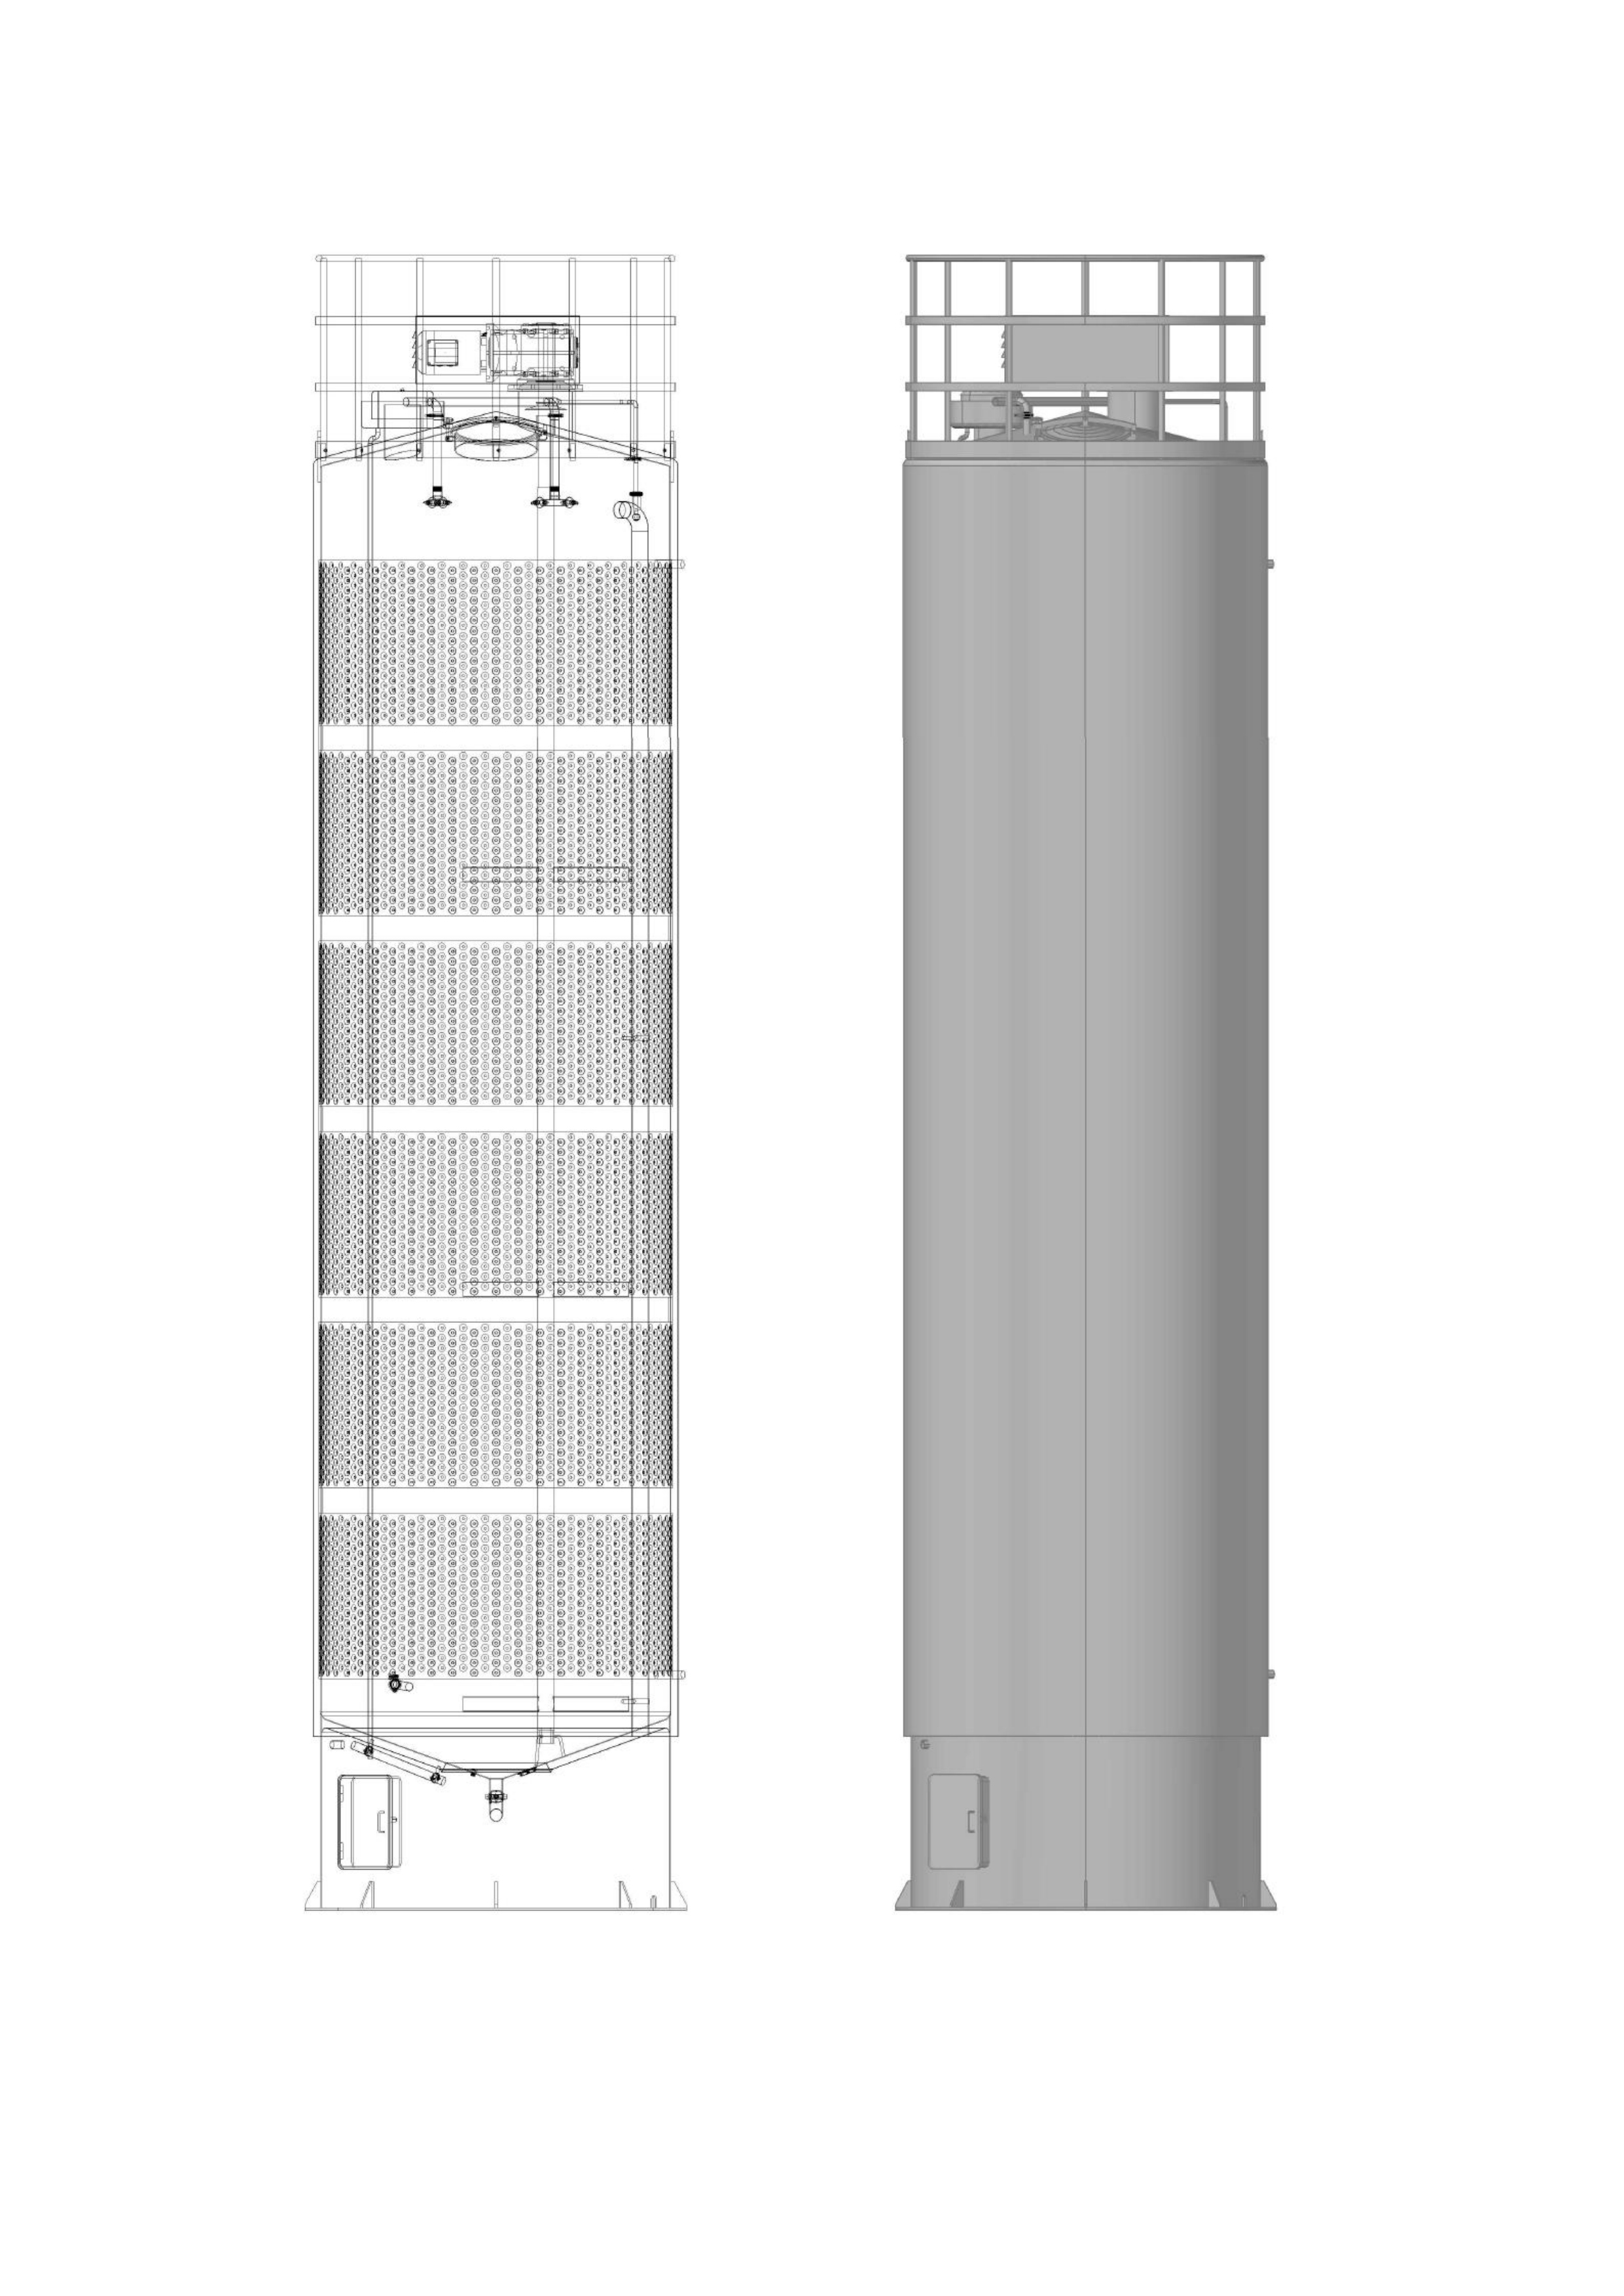
PPN engineered two jacketed mixing and storage tanks to match the customer’s egg-handling requirements. The tanks operate independently and are positioned alongside one another. Design development included revised drawings and 3D visualisation shared with the customer.
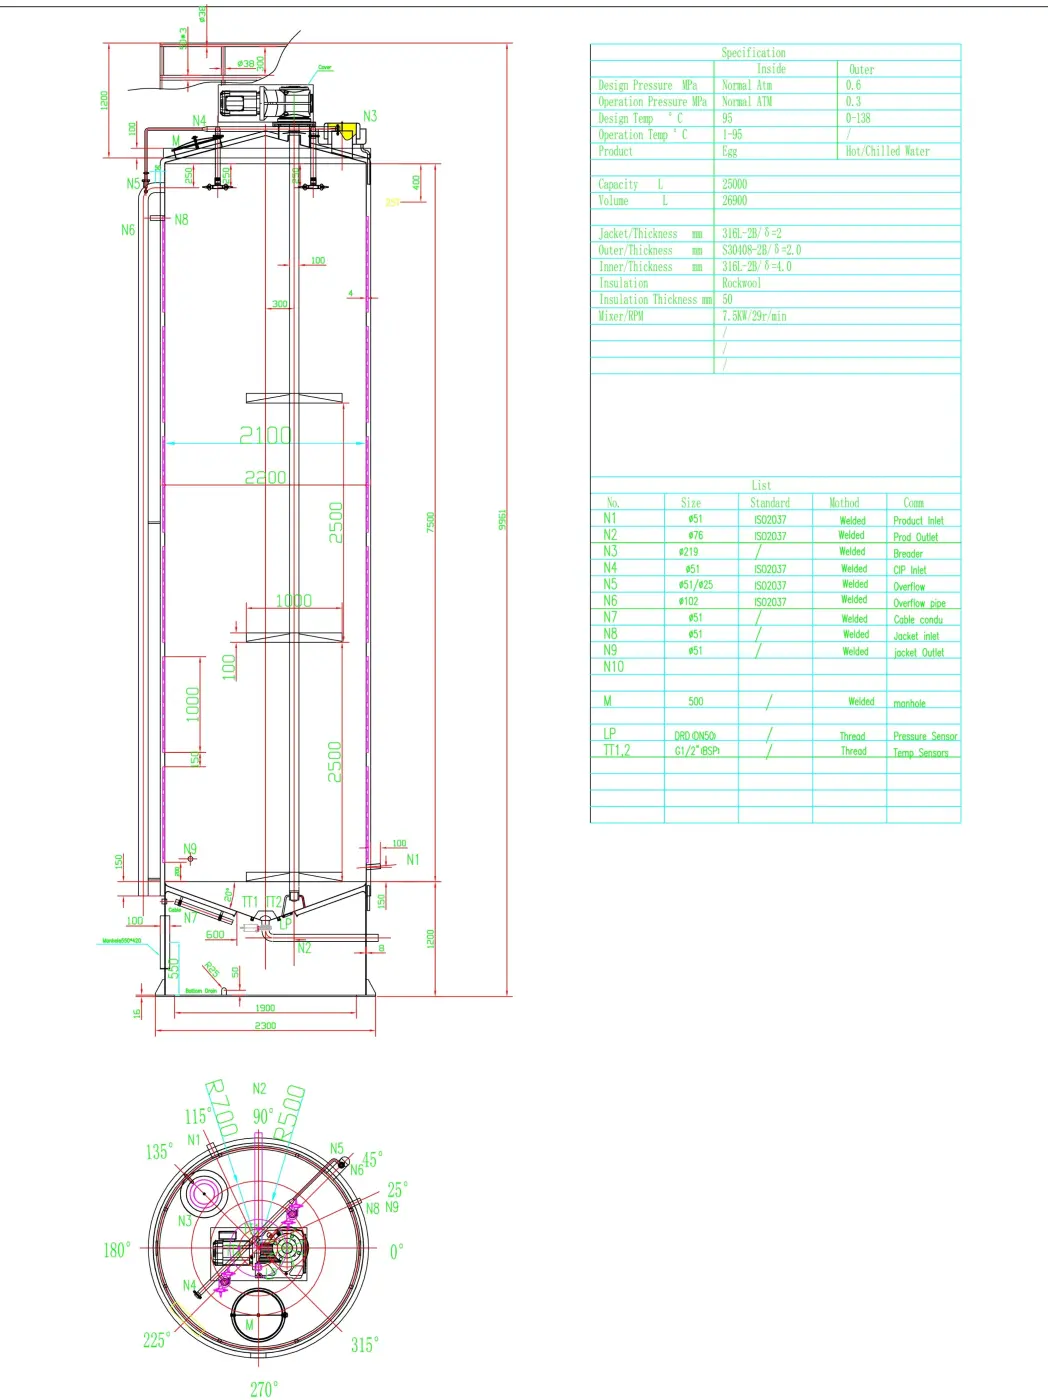
Dimple jackets provide for glycol circulation, while insulation and stainless steel cladding help limit heat gain. Gentle agitation supports even cooling and helps prevent separation. Rotary CIP spray balls provide for internal cleaning after the tanks are emptied.
System Equipment Composition
New Equipment
- Two 20,000 L working-capacity jacketed, insulated storage tanks with stainless steel cladding.
- Top-mounted stirrers with motors and gearboxes.
- Rotary CIP spray balls for internal cleaning.
- Manhole access, breather ports and engineered supports.
Customer-Supplied Equipment
- Provision for a customer-supplied bottom stirrer; PPN supplied the top-mounted stirrer.